Wafer Cleaning System Manufacturer Shares Strategies for Improving Die Yield
2026-10-17
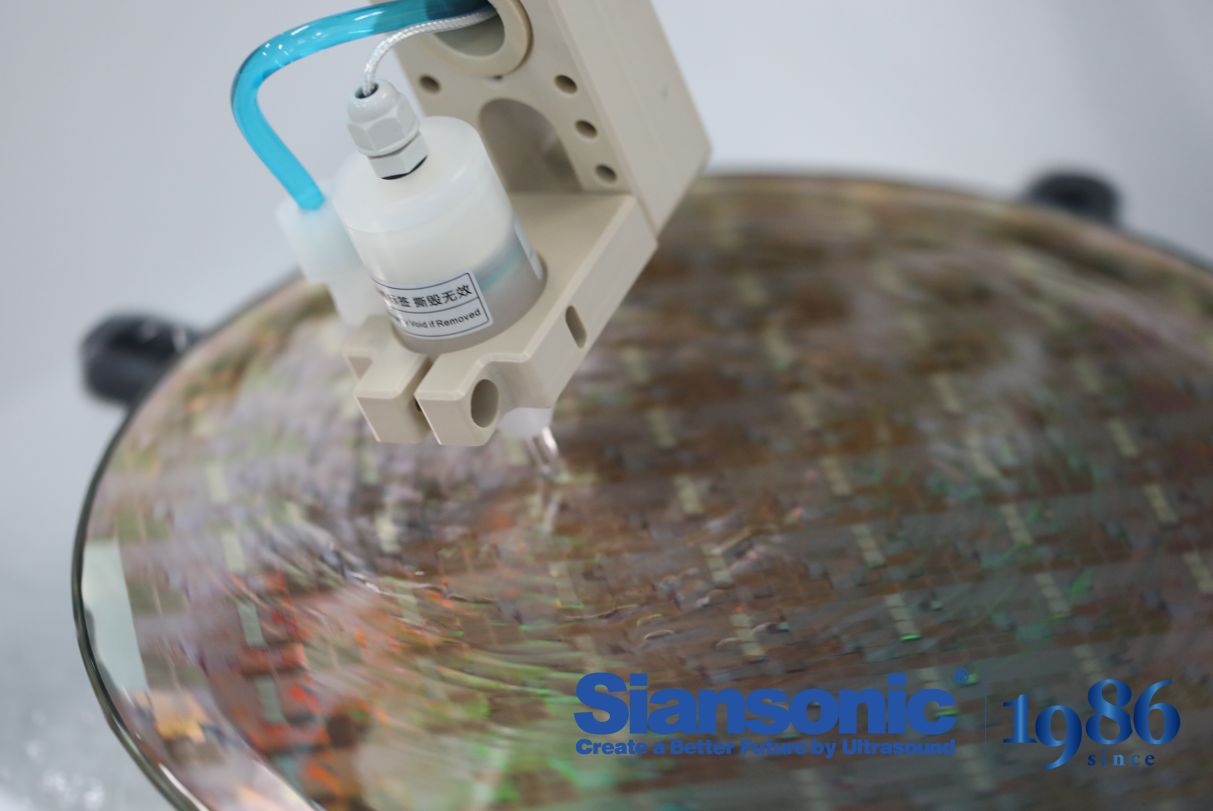
Wafer cleaning rarely gets the credit it deserves—until yield numbers start slipping. Yet as chipmakers push to smaller nodes, the difference between an average fab and an exceptional one often comes down to how well particles are removed before they become defects. That’s where Siansonic comes in. The wafer cleaning system manufacturer is opening up about the strategies that actually move the needle on die yield, from optimizing megasonic energy to rethinking chemical delivery. These aren’t theoretical concepts; they’re practical levers that could change how you approach your next process tweak.
Rethinking particle removal for advanced device geometries
Traditional particle removal relies on mechanical force or chemical dissolution, but advanced geometries such as high-aspect-ratio trenches and nanosheets create shielded regions where fluid shear and megasonic energy cannot reach effectively. As critical dimensions shrink below a few nanometers, even sub-10 nm particles can bridge conductive lines or block etching, so the margin for residue shrinks to near zero. This forces a fundamental re-evaluation of how cleaning energy is delivered into narrow, three-dimensional structures.
One emerging direction replaces blanket physical force with selective, surface-specific interactions. For example, functionalized chemistries can modulate adhesion forces so particles release only from targeted materials, while leaving fragile low-k dielectrics or ultra-thin channels intact. Another approach uses controlled cavitation or laser-induced shockwaves tuned to the resonant frequency of the particle-substrate contact, creating localized stress without pattern collapse.
The rethinking also extends to metrology and process integration. Instead of relying on post-clean defect counts, fabs are moving toward in-line monitoring of particle removal efficiency at the feature scale, using scatterometry or e-beam inspection to map residual defects inside recessed areas. This closed-loop feedback allows cleaning recipes to adapt to incoming wafer variations, shifting the goal from "clean enough" to "clean exactly where it matters."
Why your rinse water might be the biggest yield limiter
Most growers treat rinse water as an afterthought—just a quick flush to clear leftover chemistry from the spray tank. But what’s actually in that water can quietly undo weeks of careful canopy management. High pH, dissolved bicarbonates, or a sudden temperature swing can convert a perfectly stable tank mix into a sticky, ineffective residue before it ever reaches the leaf. The result isn’t always visible right away: slower uptake, uneven distribution, and a noticeable drag on yield that gets blamed on weather or genetics instead.
The real problem compounds when the same rinse cycle is reused across multiple blocks or crop stages. Each pass leaches trace elements from the equipment, dilutes the carrier, and shifts the ionic balance just enough to reduce the performance of sensitive actives like PGRs or calcium-based foliars. Over a full season, that marginal loss per application stacks up—sometimes eating away three to five percent of potential yield without a single obvious symptom. If your water source has shifted due to drought or new well depth, the issue can appear suddenly, making last year’s spray program suddenly underperform.
Pulling a water sample from the actual rinse line—not the main supply—often reveals the culprit. Bicarbonate levels above 150 ppm, pH drifting past 8.2, or even dissolved organic matter from holding tanks can all act as silent yield limiters. The fix isn’t always expensive: a simple buffering agent, adjusted rinse sequence, or switching to filtered rainwater for the final pass can recover more yield than another fungicide application. But until you treat rinse water as an input rather than a cleanup step, you’ll keep leaving bushels in the tank.
Drying without damage: solving pattern collapse in narrow trenches
Pattern collapse in narrow trenches typically occurs during the drying step, when capillary forces from the receding liquid meniscus overcome the mechanical strength of high-aspect-ratio structures. Rather than relying on lower surface tension rinses alone, a more robust approach pairs controlled evaporation gradients with a rigidifying pretreatment, such as a brief thermal cure or a self-assembled monolayer that reinforces the feature sidewalls. This shifts the failure mode from sudden snapping to gradual, elastic relaxation, preserving trench integrity even at sub-10 nm widths.
A key insight is that collapse is not purely a surface-tension problem but a stiffness mismatch between the wet and dry states. By introducing a transient supporting fluid that forms a weak gel network during the final rinse, the liquid bridge changes from a concentrated pull at the trench top to a distributed load along the entire exposed surface. The gel can then be sublimated or evaporated under near-zero capillary stress, leaving behind upright features without the usual stiction or leaning defects.
For high-volume manufacturing, the drying sequence must tolerate slight variations in trench depth, pitch, and residual moisture. A two-stage process works well: first, a low-vapor-pressure solvent reduces the meniscus curvature, and second, a brief exposure to a humidity-swing chamber causes the remaining liquid to desorb uniformly from the trench bottom upward. This avoids the random nucleation of voids that often triggers asymmetric forces, yielding a drying profile that is both repeatable and insensitive to local pattern density.
Watching contamination in real time instead of waiting for test wafers
Traditional fab monitoring relies on periodic test wafer runs that only reveal contamination after the fact, leaving hours or even days of production exposed to unknown particle levels. Watching contamination in real time flips that model by integrating in-situ sensors directly into process chambers and transfer paths, so engineers see particle counts, molecular residues, and humidity shifts as they happen. This immediate visibility means a tool can be flagged for cleaning the moment a threshold is crossed, not after a batch of scrap wafers shows the damage.
The shift from reactive test wafer analysis to live contamination tracking also reduces costly tool downtime. Instead of stopping a chamber for a scheduled monitor wafer every few lots, real-time data lets you extend productive uptime while still catching excursions early. For sensitive steps like epitaxy or gate oxide growth, even a minor particle burst can ruin yield, so watching the environment second by second allows automatic interlocks to pause processing before the next wafer enters a compromised zone.
Beyond yield protection, real-time contamination monitoring builds a historical fingerprint for each tool. That fingerprint helps maintenance teams spot gradual drift—like a slowly degrading O-ring or a pump-backstreaming issue—long before it becomes a full-blown particle storm. By replacing slow, periodic test wafer checks with continuous environmental awareness, fabs can respond to contamination in minutes rather than shifts, preserving both throughput and device reliability.
Fine-tuning chemical mixtures to keep metals off the wafer
Getting metal ions off a wafer after etch or CMP isn't just about adding more chelator. The real work happens in adjusting the redox potential so copper, cobalt, or titanium stays in solution long enough to be rinsed away. A shift of 0.1 in pH or a small change in ligand ratio can flip a recipe from clean to contaminated.
Many fabs spike in a secondary complexing agent that competes for the same metal sites but has a weaker hold. This prevents the primary chelator from pulling metals back onto hydrophobic low-k surfaces during the spin-off step. Electrochemical noise and TXRF feedback show which metals are actually leaving the wafer, not just being redistributed.
Oxidizer concentration matters more than most people assume. A slightly stronger peroxide or peracetic dose can passivate the metal surface, but too much creates rough oxide growth that traps particles. The goal is a narrow process window where etch rate stays low, the barrier stays intact, and final metal counts drop below detection without damaging sensitive dielectrics.
When the cleaning tool needs its own cleaning schedule
It’s easy to forget that the sponge scrubbing last night’s sauce or the mop gliding across kitchen tiles picks up more than just visible grime. A damp sponge left on the sink ledge becomes a cozy home for bacteria within a day or two, and a mop head that never dries thoroughly starts to smell like a forgotten gym bag. These tools don’t just get dirty—they get colonized, and using them again simply spreads the problem around.
A practical rhythm helps. Swap or sanitize kitchen sponges every three to five days—microwave damp sponges for one minute or run them through a hot dishwasher cycle. Wash microfiber cloths and mop heads after each heavy use, and let them dry completely before storing. For vacuums, check the brush roll for hair weekly and rinse washable filters monthly; a clogged filter forces the motor to work harder and blows fine dust back into the room.
The payoff isn’t just hygiene—it’s performance. A clean mop lifts grime instead of smearing it, and a vacuum with clear airflow actually picks up debris instead of scattering it. Treat the cleaning schedule for your tools as seriously as the cleaning schedule for your home. Ten minutes a week spent on the tools themselves saves hours of ineffective scrubbing later.
FAQ
We rely on a combination of megasonic energy and dilute ammonia-peroxide mixtures. The megasonic transducer array is tuned to create controlled cavitation at the wafer surface, which dislodges particles down to 0.1 micron without damaging fragile structures. The chemistry ratios are adjusted in real time based on incoming particle counts.
Our systems use a hot IPA vapor dry with a gradual pull-out velocity profile. Instead of a single fixed speed, the wafer is withdrawn through a temperature-controlled vapor zone at a rate that slows near the liquid-vapor interface. This reduces surface tension gradients and minimizes watermark defects on high-aspect-ratio features.
We use inline conductivity and optical sensors to monitor bath chemistry every 30 seconds. When concentration drifts beyond a narrow band, the system automatically bleeds and feeds fresh chemicals. This prevents the gradual buildup of dissolved silicon and trace metals that can re-deposit on wafers and kill yield.
For nodes below 28nm we recommend non-contact cleaning modules only. Our brush scrubbers are reserved for thicker films or backside clean where contact damage risk is minimal. The frontside uses high-frequency acoustic streaming and a low-pressure liquid jet, so there is no direct mechanical contact with the device side.
We suggest replacing point-of-use filters every 500 wafer passes or 72 hours of operation, whichever comes first. Recirculation pump impellers and O-rings should be inspected monthly for wear particles. A quick daily check of pressure differentials across filters often catches degradation before it impacts bath cleanliness.
There are pre-programmed recipes for common stacks like copper/low-k, aluminum, and polysilicon. Each recipe adjusts pH, temperature, and megasonic power. For sensitive materials, we use a short pre-rinse with CO2-dosed DI water to prevent copper oxidation, then a low-energy clean that avoids galvanic corrosion.
Track particle counts before and after clean, chemical bath lifetime, megasonic power draw, and rinse water resistivity. Correlating these with final probe yield often reveals a specific threshold—for example, when post-clean particle counts exceed 15 adders per wafer, yield drops sharply. That allows fabs to set tighter SPC limits on the cleaning step.
Conclusion
Wafer cleaning system manufacturers are pushing fabs to abandon blanket particle removal recipes for advanced device geometries. High-aspect-ratio structures trap residues that conventional megasonic or spray cleaning cannot reach, so the focus has shifted to geometry-aware energy delivery and chemistry that wets deep trenches without leaving films. Rinse water gets far less attention than it deserves; trace organics, dissolved oxygen, and even static charge in ultrapure water can redeposit particles or create pits. The vendor recommends inline sensors for resistivity, TOC, and temperature at the point of use, not just at the central plant. Drying is where many good cleans fail. Narrow trench patterns collapse under capillary force when water evaporates, so low-surface-tension solvents and controlled vapor drying have become standard for fragile layers.
Test wafers after the fact are no longer enough. Real-time contamination monitors now track particle counts, metal ions, and organic films during the clean itself, letting engineers tune the process before a lot is at risk. Chemical formulations are being adjusted with selective chelators and low-etch additives to keep copper, aluminum, and other metals off the wafer surface without attacking exposed dielectrics. The cleaning tool itself also needs a scheduled self-clean cycle; residue buildup inside chambers and lines can shed particles back onto wafers and undo all the upstream work. Tying these practices together—geometry-specific particle removal, strict rinse water control, damage-free drying, inline sensing, tailored chemistry, and tool hygiene—gives fabs a practical path to higher die yield without adding process steps that slow throughput.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/