Low-Dew-Point Wheel Desiccant Dehumidifier Unit Manufacturer Reveals Critical Design Factors for Deep Drying Systems
2026-11-02
Achieving a stable low dew point in deep drying is a different game than standard dehumidification. Airflow, regeneration temperature, rotor design, and leakage control all interact in ways that are easy to get wrong. ROTER, a dedicated wheel desiccant dehumidifier unit manufacturer, pulls back the curtain on the critical design factors that determine whether a system delivers reliable ultra-dry air or quietly drifts off spec.
Rotor Construction Details That Make or Break Deep Drying
The real difference between a rotor that merely moves material and one that drives moisture out lies in the internal vane geometry. Curved, overlapping lifters that create a dense cascading curtain across the full cross-section outperform straight radial flights every time. If the flights are too shallow or spaced too far apart, product clumps and slides rather than tumbles, leaving wet pockets that survive multiple passes through the heat zone.
Another underappreciated detail is the rotor cone angle and the clearance at the discharge end. A slight taper combined with an adjustable weir plate lets you hold material in the hot airstream longer without choking airflow. Weld placement matters too — rough, proud welds on flight edges snag fibers and fines, which then char and block the very paths intended for vapor release. Polishing those transitions and using abrasion-resistant liners only where wear actually occurs keeps the rotor open and predictable.
Finally, the shell thickness and stiffener ring pattern determine whether the rotor stays round under thermal cycling. A thin shell with widely spaced rings will breathe and flex, cracking the internal welds and creating bypass channels for hot gas. Deep drying demands a rotor that holds its shape at sustained temperature, because any gap between flight tip and shell becomes a shortcut for heat that never touches the product.
How Small Leaks in the Purge Sector Undo Low Dew-Point Performance
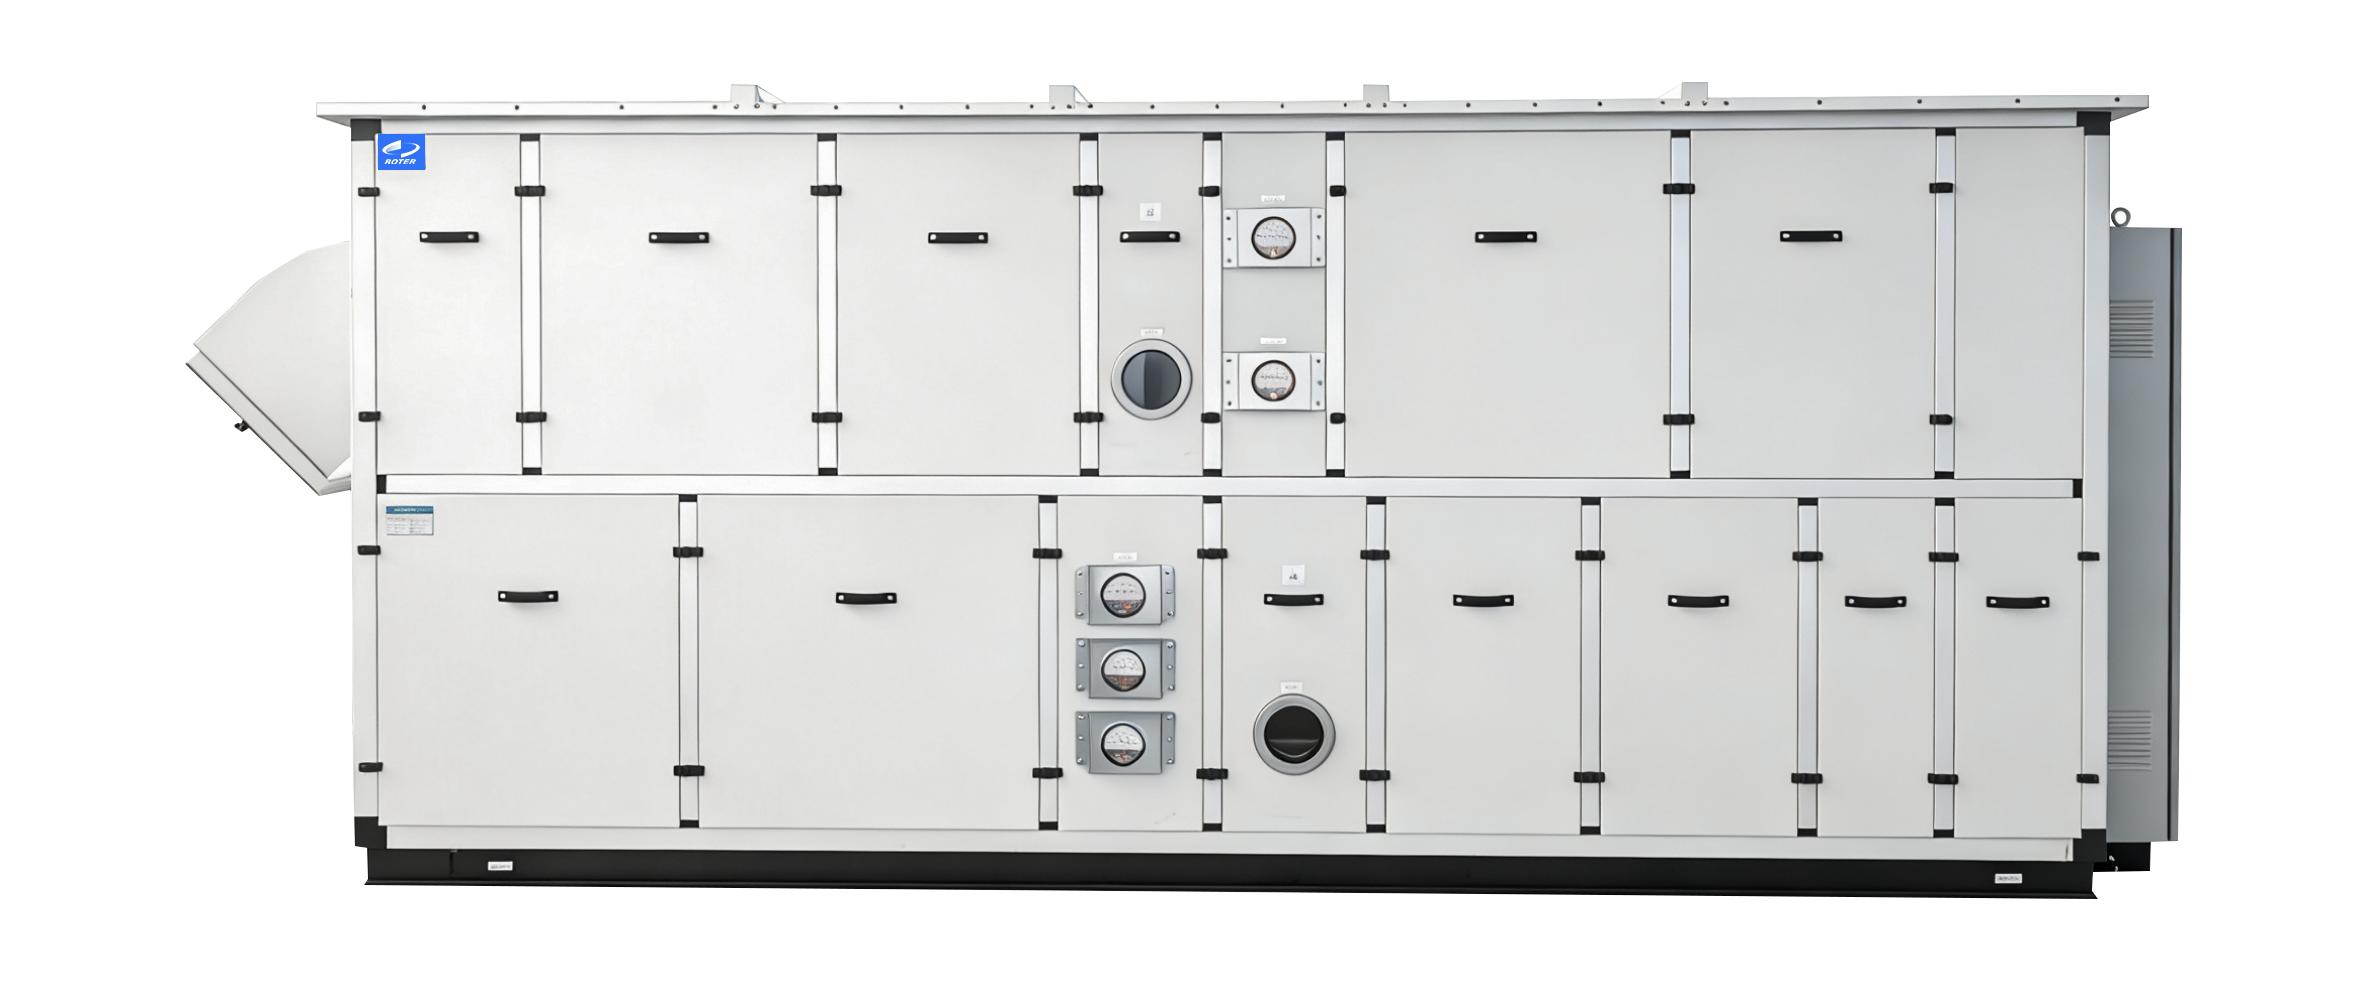
The purge sector in a desiccant dryer is supposed to be a closed loop of regenerated air, but even a pinhole-sized defect can quietly undo months of dew-point tuning. Technicians often chase sensor drift or heater output while the real culprit is a hairline crack near a weld or a slightly loose fitting that lets ambient air slip into the purge stream. Because purge air is meant to carry moisture away from the desiccant bed, any outside air entering at this stage adds humidity precisely where it should be removed.
The failure mode is subtle because the pressure differential across the purge sector is often less than a few inches of water column. A small leak doesn't create an audible hiss or a visible condensation trail; instead, it raises the dew point by only two or three degrees at first. Over time, moisture accumulates in the desiccant pores, reducing the bed's capacity to dry the process air. The dryer then compensates by cycling the heater more frequently, which masks the leak as a demand-side issue and drives up energy costs.
What makes these leaks particularly insidious is that they rarely show up in standard maintenance checks. Bubble tests miss them because the leak path is often micro-capillary, and ultrasonic detectors can't distinguish a minor leak from normal valve actuation noise. The only reliable detection is a deliberate pressure-decay test on the isolated purge circuit, combined with a dew-point trend that refuses to stabilize at the expected setpoint. Until those steps are taken, low dew-point performance remains a moving target.
Desiccant Flute Depth Is Not Just a Geometry Choice
Flute depth in a desiccant rotor tends to get treated as a line-item dimension, but it quietly sets the rules for air-to-desiccant contact. A deeper profile can carry more coating, yet that alone rarely means lower dew point. What changes first is residence time and moisture diffusion through the channel; past a certain depth, the inner coating sees less active air, while pressure drop climbs enough to make the added capacity pointless.
Shallow flutes move air faster and usually reduce the energy demand on the fan, which matters in retrofit jobs where duct pressure is already limited. The catch is less desiccant mass and a narrower regeneration window. Tuning flute depth to the actual humidity load, face velocity, and cycle time almost always beats copying a standard geometry from a datasheet. That is why the choice is really an operating decision disguised as a dimensional one.
The Regeneration Loop Needs a Thermal Buffer, Not Just a Heater
A common mistake in regeneration loop design is treating temperature control as a simple on-off problem. You install a heater, set a target, and expect the bed to follow. But real packed beds, catalysts, and adsorbers have significant thermal mass of their own, and the heat front moves slowly. Without a buffer, the inlet gets scorched while the outlet barely warms up, and when the heater cycles off, cold gas quenches the reaction before it finishes.
Adding a thermal buffer changes the dynamic entirely. A block of high-heat-capacity material placed downstream of the heater absorbs the initial spike, then releases that energy over a longer window. This allows the regeneration front to travel at a steadier pace, avoiding both incomplete burnout at the tail end and thermal cracking near the inlet. The heater still supplies the same average energy, but the buffer converts a jagged temperature trace into a smoother, more controlled ramp.
The payoff becomes obvious during partial-load or intermittent operation. A bare heater has to be sized for the coldest conceivable condition, which means it runs at a fraction of its rating most of the time. A buffer lets you run a smaller heater continuously, storing surplus heat when demand is low and releasing it when flow surges. That reduces cycling stress on heating elements and keeps downstream components from seeing repeated thermal shocks.
Sensor Placement Determines How Reliable Your Dew-Point Reading Really Is
A dew-point sensor tucked into a dead corner of a compressed air line won't see the same moisture conditions as the air that actually reaches your process. Even a few feet of distance, a low point that collects condensate, or a stretch of pipe with different thermal mass can create a reading that looks stable but has little to do with what's happening downstream.
Placement near elbows, filters, dryers, or areas with restricted flow tends to produce readings that lag or spike unexpectedly. The sensor only knows the microclimate it sits in. If that spot traps moisture or experiences temperature swings, the dew-point value becomes a reflection of the installation rather than the gas stream itself.
For a reading you can actually trust, the sensor needs to see representative flow, not a stagnant pocket. That usually means a location with steady velocity, minimal dead volume, and no chance of liquid water pooling around the probe. Get the placement wrong and even a high-end sensor will confidently report a number that misleads your entire moisture control strategy.
Long-Term Low-Dew-Point Operation Hinges on Seal Material Selection
In low-dew-point systems, even a few parts per million of moisture can compromise product quality or accelerate corrosion, so the sealing elements become the quiet gatekeepers of long-term stability. Elastomers that perform well at ambient humidity often falter when the surrounding air is stripped down to a bone-dry state—they lose plasticizers, turn brittle, or develop microcracks that invite leakage. Selecting a seal material isn't just about matching temperature ratings; it's about understanding how the polymer network behaves when there's almost no water vapor left to act as a subtle lubricant or plasticizer.
Perfluoroelastomers and certain high-performance fluorocarbons hold up better than generic nitrile or silicone in these harshly dry environments, but even among these, filler types and cure systems matter. A poorly chosen carbon black or a sulfur-cured backbone can release trace volatiles or degrade through oxidation, slowly poisoning the very dryness the system is designed to maintain. Field data from compressed air dryers and semiconductor gas cabinets often shows that seal-related failures happen not at startup, but after months of continuous sub-zero dew-point exposure—proving that material selection is a marathon decision, not a sprint.
Engineers who treat the seal as a consumable commodity tend to chase recurring leaks and unplanned downtime. A more practical approach involves evaluating compression set, outgassing rates, and low-temperature elasticity under the actual moisture conditions of the process—not just the datasheet values. Pairing the right elastomer with a well-designed gland geometry and a clean, dry assembly environment extends the interval between rebuilds drastically, turning a chronic headache into a background reliability metric.
FAQ
Conventional refrigerant units struggle below 50% RH because coil frost limits moisture removal. Wheel desiccant systems use a rotating silica gel or molecular sieve matrix to adsorb water vapor directly, which allows stable operation down to -60°C dew point. The key is the rotor's ability to create a vapor pressure gradient independent of dew point, not just cooling capacity.
The desiccant loading per square meter of rotor face, the flute geometry for laminar airflow, and the thickness of the adsorption zone. A rotor with higher active desiccant content but poorly shaped flutes will actually perform worse due to channeling. We also tune the regeneration sector angle—typically 90 to 120 degrees—to balance moisture carryover and heat input.
It is often the difference between hitting -40°C and -70°C dew point. A 2-millimeter gap in the rotor housing can leak 5–8% of untreated process air into the dry stream. We use double-lip brush seals and a positive-pressure purge zone to minimize cross-flow. Without that, the rotor's adsorption capacity is wasted.
A single wheel can reach about -40°C dew point if the rotor is deep enough and regeneration temperature is high. To go below that, you need a dual-rotor cascade or a pre-cooling coil upstream to drop moisture load. Our deep drying systems often pair a first-stage rotor with a second polishing rotor and a post-cooler, especially for lithium battery dry rooms.
Regeneration consumes 70–80% of total energy in a desiccant unit. We avoid constant high-temperature regeneration because it bakes the desiccant and shortens rotor life. Instead, we use a variable-temperature profile: high heat only in the first third of the regeneration sector, then lower heat to finish desorption. This cuts energy use by up to 25% without affecting outlet dew point.
Most failures come from desiccant contamination or rotor face saturation. Oil aerosols, acidic gases, or fine dust in the process air blind the micropores. We specify a two-stage filtration train—MERV 8 prefilter plus F9 final filter—and add a washable rotor option. Another common issue is sensor drift; the dew point transmitter must be calibrated against a chilled mirror reference every six months.
You cannot size by room volume alone. The critical inputs are the internal moisture load from personnel, door openings, and product off-gassing, plus the target dew point differential. We calculate the required dry air flow in cubic meters per hour using a psychrometric model, then apply a safety factor of 1.15–1.25 for rotor aging. An oversized unit will cycle too often and actually raise the average dew point.
Check rotor rotation speed monthly—slippage of the drive belt can drop dew point performance by 10°C. Clean the purge air filter quarterly. Inspect seal wear every 2,000 operating hours. Also monitor the regeneration outlet temperature; if it rises above 65°C, it means the desiccant is not releasing moisture efficiently, which points to a clogged rotor or reduced airflow.
Conclusion
Deep drying with a low-dew-point wheel desiccant dehumidifier is rarely decided by the desiccant alone. A manufacturer working in this niche points to rotor construction as the first differentiator: how the desiccant is bonded, the uniformity of the wheel's sectors, and the tolerances that keep regeneration air from bleeding into the process stream. Small purge-sector leaks are notorious for undoing low dew-point performance because even a fraction of humid regeneration air re-entering the dried air raises moisture levels beyond specification. Flute depth adds another layer of complexity. It is not just a geometric choice but a direct lever on contact time, face velocity, and pressure drop. A flute that is too shallow lets air pass before deep moisture adsorption occurs; one that is too deep increases energy consumption and can leave the regeneration side under-heated. Some manufacturers address this with variable flute depth or layered desiccant zones, matching the rotor to the final moisture target instead of relying on a standard off-the-shelf profile.
On the regeneration side, a thermal buffer matters more than heater capacity. Without buffering, the regeneration air temperature oscillates with load changes, causing incomplete desiccant drying and moisture carryover. A buffer smooths these swings and keeps the desiccant at a consistent regeneration temperature. Dew-point sensor placement then determines whether operators can trust the reading at all. Probes fitted near elbows, in laminar pockets, or too close to the rotor often report a dew point that does not reflect the delivered air. Reliable low-dew-point systems place sensors in fully mixed, representative locations with minimal lag. Finally, long-term performance depends heavily on seal material selection. Seals around the rotor and between process, purge, and regeneration sectors face hot, humid air and dry air cycles. Elastomers that harden or shrink open internal leakage paths, slowly raising the output dew point even when the rotor remains healthy. Selecting low-outgassing, compression-set-resistant seal materials and replacing them on a conservative schedule keeps sector isolation intact over years of continuous duty.
Contact Us
Contact Person: Rhea
Email: [email protected]
Tel/WhatsApp: +8618800560886
Website: https://www.rotorairtech.com