Custom CNC Machining: Precision Solutions for Complex Parts
2026-11-16
When a design calls for complex parts with tolerances measured in microns, standard machining falls short. Custom CNC machining is where precision meets possibility—and at Tianyu, that intersection is built into every setup. Here’s what separates true precision solutions from the rest.
When the Print Says ±0.0005, We Don't Flinch
A tolerance like ±0.0005 usually makes people pause. In our shop it doesn't, because the first thing we do is check how the part will move when it heats up, how the tool will deflect under load, and where the measurement will actually land. That number is not a guess; it's a range we've already mapped out before the spindle starts.
We don't flinch because the process is built backwards from the tolerance. If the print says five tenths, we know the tool needs a certain corner radius, the coolant needs to stay at a steady temperature, and the inspection has to happen with the same reference points every time. The tolerance isn't a threat—it's just a spec that tells us which routine to use.
Deep Pockets, Thin Walls, No Drama
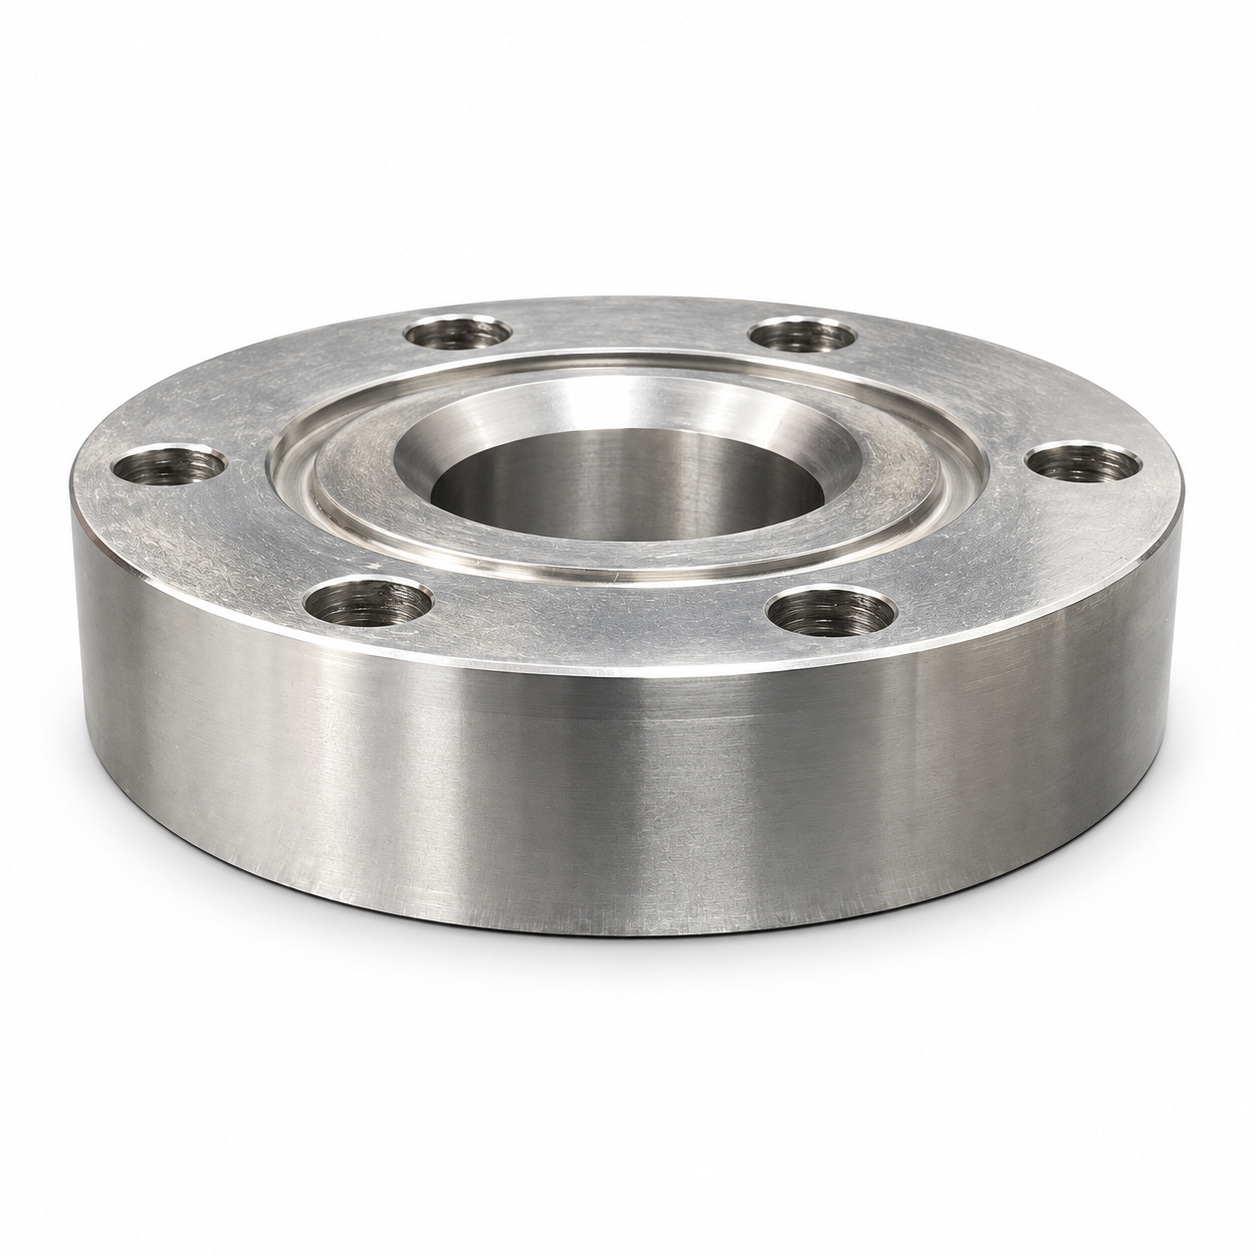
You don't have to flaunt a healthy bank balance to enjoy a place that feels quietly expensive. Here, the money went into the details you touch every day—solid hinges, warm light, a kitchen that actually works—not into marble foyers meant to impress the delivery guy.
Yes, the walls are thin. That means you'll hear the occasional kettle click or a neighbor laughing at something on TV. It also means you're never sealed off in some sterile box. The trade-off is a kind of honesty: you live among people, not above them.
And nobody has time for drama. The building attracts a certain type—people who've done well enough to afford better but choose this because it's real. They keep odd hours, mind their own business, and say hello in the stairwell. That's the whole deal.
Programming Around the Part's Personality
A blank of 6061 aluminum never behaves like the CAD model suggests. Run your finger across its surface after a facing pass and you’ll feel a slight dish, a witness mark from a dull insert, or a hard spot near a corner that deflects the tool. Programming around the part’s personality means reading these physical cues before writing a single line of G-code. Instead of trusting the blueprint’s uniform wall thickness, you probe the actual stock, map the rough spots, and choose tool engagement angles that keep the cutter from grabbing where the material is softer.
Thin ribs will ring at 4,000 RPM but stay quiet at 3,600. A deep pocket that holds coolant differently than expected demands a chip-breaking peck cycle rather than a continuous helical ramp. We often rough one side of a casting with conventional milling to avoid lifting a fragile edge, then switch to climb milling on the opposite side where the mass is thicker. The part’s personality emerges from asymmetry, residual stress, and how it was fixtured last week. Respect those quirks and you get a stable cut; ignore them and you chase chatter marks for an afternoon.
The real test happens at the first article. Stand near the enclosure, watch the chip color shift from silver to straw, listen for the low thrum that signals a load spike. Maybe the tool needs a 0.005-inch radial engagement reduction on the third pass because the part relaxes after the second. That’s not a compromise, it’s the difference between running blind and running with your hands on the machine. Programming around a part’s personality turns a mediocre process into one that holds tolerance without babysitting.
Materials That Fight Back, Machined Anyway
Some alloys seem to have a grudge. They work-harden the instant a cutter touches them, throw off jagged chips that scour the tool edge, and vibrate like a plucked string the moment you back off the feed. Yet they still get machined—not by overpowering them, but by listening to what the material is trying to say.
The trick is rarely a single magic insert grade or a secret speed. It’s a combination of deliberately unglamorous choices: a negative rake that bullies the chip into breaking, a lower spindle speed that keeps heat in the chip instead of the workpiece, and a toolpath that never lets the edge linger in one spot long enough to build up a wear scar. When the material fights, you stop forcing it and start maneuvering.
In practice, that means checking the edge under a loupe every few parts, adjusting the coolant nozzle until the stream hits the exact root of the cut, and sometimes accepting a shorter insert life as the price of getting a clean, dimensionally stable part out of a block of stubborn metal. Machining these materials isn’t about winning the argument—it’s about finishing it.
Small Batches, Big Expectations
There’s a quiet confidence that comes from working in small batches. It’s not about scarcity for its own sake—it’s about giving each unit enough attention to catch the flaws that mass production would never notice. Every run becomes a conversation between the maker and the material, and that dialogue shapes what ends up in your hands.
Expectations rise when volume drops. A limited run can’t hide behind averages or acceptable margins. If one batch falls short, the whole story falls short. That pressure pushes us to test more, adjust more, and sometimes start over entirely rather than ship something that simply meets the minimum.
The result is a product that feels less like an output and more like an answer—to a specific problem, a particular palate, or a moment that deserved better than the generic. Small batches don't guarantee perfection, but they make it impossible to ignore the details that bigger operations leave behind.
The Difference Is in the Details You Can't See
Most people only notice what a product looks like on the surface. The real distinction, though, lives in the choices that never get photographed. A slightly denser foam, a hinge tested past a hundred thousand cycles, a coating that resists fingerprints without changing the texture. Those are the things you feel after six months, not on day one.
It’s easy to copy a silhouette. It’s much harder to match the hours spent adjusting internal tolerances or replacing a cheaper component that no one would have complained about. That quiet obsession is what separates something that simply works from something that keeps working in ways you can’t point to.
The result is rarely dramatic. It won’t show up in a side-by-side photo. But after enough use, you stop thinking about the object itself because everything about it fits your hand, your routine, your expectations. That absence of friction is the detail you can’t see, and it’s the one that matters most.
FAQ
We take your CAD model and turn it into a finished part using multi-axis milling, turning, or wire EDM. That means undercuts, deep pockets, threaded holes, and tight-fit features are all fair game.
Typical tolerance is ±0.005 in, and we can hold ±0.001 in on critical features when the material and setup allow it. We'll flag any areas where your design asks for more than the process can reliably deliver.
Aluminum 6061 and 7075 are popular for their stability, but we also machine stainless steels, titanium, brass, and engineering plastics like PEEK or Delrin. The best choice depends on strength, weight, thermal needs, and whether the part gets anodized or coated later.
Yes, with 5-axis positioning or clever workholding we often avoid extra setups. If a feature is truly unreachable, we'll suggest a small design tweak—like a relief or split line—so you still get the function without paying for exotic tooling.
A STEP or IGES file works best, along with a PDF drawing that calls out tolerances, surface finish, and any critical dimensions. If you only have a sketch or a broken sample, we can reverse-engineer it too.
No hard minimum. We regularly run single prototypes, and our setup process is streamlined enough that 10- to 100-piece batches stay cost-effective without dedicated hard tooling.
Absolutely. Bead blasting, anodizing (Type II or III), electropolishing, powder coating, and heat treating are all available. We can match a specific color or surface roughness if you provide a reference.
Prototypes usually ship in 5-10 business days. Short production runs might take 2-4 weeks, depending on the number of features, material availability, and any secondary finishing steps.
Conclusion
Tolerances like ±0.0005 aren't a reason to hesitate—they're the baseline. Deep pockets, thin walls, and awkward internal features get programmed around the part's actual behavior, not just the CAD model. Toolpaths are adjusted for how the material moves, how it heats up, and where it wants to spring back, so the first article comes off the machine ready to inspect, not ready for a list of excuses. Whether it's a short run of five or fifty, every setup gets the same scrutiny as a production job.
Some materials fight back—titanium, hardened steels, glass-filled polymers—but that just means feeds, speeds, and coolant strategies get dialed in until the cutting is quiet and the finish is clean. The real difference shows up in the details you can't see from the outside: deburred intersections inside deep bores, consistent wall thickness where nobody will measure unless they cut it apart, and a surface finish that holds a coating without extra prep. It's not about hitting the print once; it's about making sure every feature, even the hidden ones, would pass inspection twice.
Contact Us
Contact Person: Vera Yao
Email: [email protected]
Tel/WhatsApp: 8618512832770
Website: https://www.tianyucnc.com