Chocolate Enrober Vendor Checklist for Choosing the Right Equipment Partner
2026-11-16
Choosing a chocolate enrober supplier is rarely just about the machine. It is about who stands behind it when production schedules tighten or a batch does not coat the way it should. Many buyers compare spec sheets, but few start with the practical questions that separate a responsive partner from a distant vendor. In this checklist, we look at what actually matters before you commit. Whether you are upgrading a single line or planning a full-scale confectionery expansion, GUSU has learned that the right equipment partner is often the difference between smooth commissioning and months of troubleshooting.
Spend Time with the Machine Before You Talk Numbers
Most people ask for the spec sheet first. They want cycle times, output rates, and energy draw before they have even seen the machine run. That sequence misses a lot. Stand next to it while it starts up. Listen to the way the motor settles into idle. Put a hand on the frame when it is working. The numbers will not tell you that a guard rattles at full speed or that the emergency stop is awkward to reach, but those details shape every shift.
Run the machine the way your crew actually would, not the way a demo script suggests. Load it, unload it, make the small adjustments you know will be necessary. A rated speed can look impressive while the real cycle gets eaten by tool changes, cleaning, or a poorly placed control panel. Once you have spent thirty minutes with it, you start to notice which numbers matter and which ones are just decoration.
That time also changes the conversation later. Instead of negotiating from a brochure, you are negotiating from experience. You can push back on claims that feel optimistic and accept compromises that will not hurt daily work. By the time the figures come up, they are not abstract targets anymore. They are either consistent with what you felt and saw, or they are not.
Ask What Happens When the Chocolate Doesn't Behave
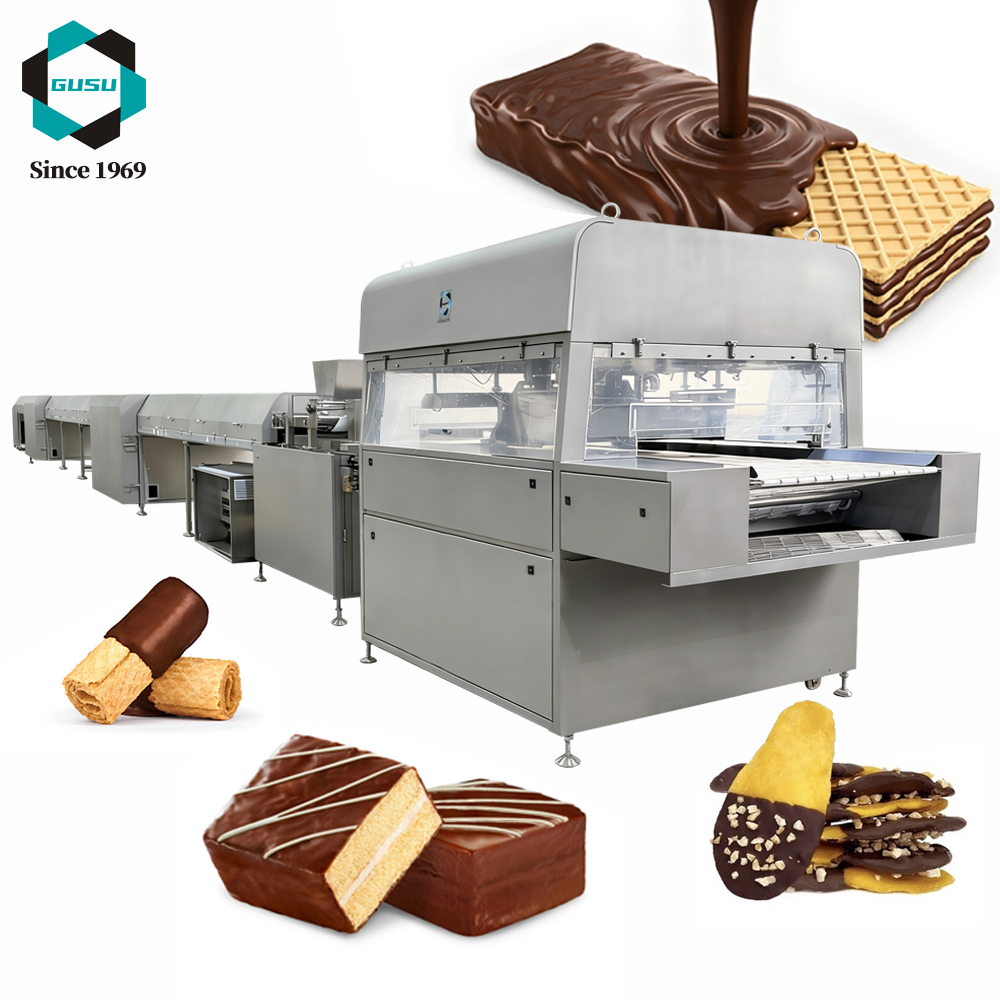
When a batch of chocolate turns streaky, dull, or refuses to set, the first useful move is not to rush for a fix. Instead, ask what the chocolate is actually doing. Did it get too hot over the double boiler, or did a few drops of water sneak in while stirring? Sometimes the answer sits in a small detail: a humid kitchen, a thermometer that drifted out of calibration, or couverture that was never brought up to the right working temperature.
Treat the failed batch like a short investigation. Write down the room temperature, the type of chocolate, and how long it spent melting. If it seized, think about whether the bowl or spatula was completely dry. If it bloomed after setting, consider whether it cooled too slowly or sat in a warm spot. The habit of asking what changed rather than blaming the chocolate usually reveals a pattern you can adjust next time.
This kind of questioning also saves perfectly usable chocolate from the bin. A gray cast on the surface may look like a mistake, but it often just means the cocoa butter moved to the surface. That bar can still be melted down for ganache or baking. The point is to learn what the chocolate is telling you before deciding whether to rescue it or start over.
Check How Many Parts Hide Behind the Service Panel
Before you order a single replacement switch or clip, take a close look at what actually sits behind that removable cover. Many machines pack more than just the obvious connectors and fuses back there—often a hidden relay, a spare wiring harness, or even a small control module gets tucked away without any mention in the quick-start guide. Removing the panel usually reveals a dense cluster of parts that rarely get checked during routine cleaning, so it pays to photograph everything before touching a single screw.
A practical way to avoid surprises is to compare the physical count against the exploded diagram in the service manual. Count each terminal block, cable tie anchor, and rubber grommet individually; don’t assume that two similar looking brackets mean identical hardware behind them. You might find that a secondary fuse holder or a diagnostic port sits behind a lower lip that only becomes visible once the panel is angled outward and slid to the side.
Finally, make a quick list of parts that are secured from the back rather than the front, since those are the ones people forget to reinstall or accidentally damage when forcing the cover closed. A small inspection mirror and a flashlight help spot parts tucked above eye level, behind brackets, or below the main wiring loom. Taking ten minutes to check what’s actually back there can save you from ordering the wrong part or discovering a broken clip only after the machine refuses to start.
Find Out Who Actually Answers the Phone on a Friday
Friday after 2 p.m. has a way of separating companies that mean it from the ones that just say it. A quick call to a main line or a direct extension tells you more than any polished pitch deck ever will. If a real person picks up on the second ring and sounds present, that is a signal. If you get a voicemail maze or an auto-attendant that pretends to care, that is a signal too.
Try it with a handful of names on your list. Don't schedule it, don't warn them. Just call. The pattern you notice might surprise you: some of the busiest people still answer, while some "always available" teams vanish by noon. It is not about catching anyone out; it is about seeing who treats the end of the week as part of the actual week.
Once you spot the ones who pick up, hold on to them. Responsiveness on a Friday is rarely an accident. It usually means the person has enough control over their workload, enough respect for the caller, or enough pride in the work to stay engaged when the week is wrapping up. That is a quality worth remembering.
Compare Cleaning Downtime, Not Just Coating Speed
Most datasheets highlight how fast a coating can be applied, but real production lines tell a different story. A machine that sprays quickly yet forces you to stop for an hour between color changes drains more capacity than a slightly slower unit with rapid purge cycles. Look beyond the headline speed number and ask how long the system actually sits idle during cleaning, flushing, and material switches.
Some manufacturers quote cleaning times only for a single standard color, ignoring what happens with high-solid primers or waterborne clears. Others require manual scrubbing of nozzles and lines after every batch, which adds unpredictable labor to each shift. Compare the full downtime sequence side by side, from the moment the last part exits the booth to the moment the next color is ready to spray. A few extra minutes saved per changeover can add up to dozens of extra production hours over a month.
Field reports often reveal that automated purge and solvent recovery systems pay for themselves quickly, even if the initial coating speed looks average. When you evaluate equipment, request video or live demos showing realistic changeovers with the actual materials you use. The coating speed only matters during the time the gun is moving; everything else is downtime you are paying for.
Visit a Running Line and Listen to the Operators
Standing beside a line that is actually running changes the questions you ask. The operators do not describe the machine from memory; they lean toward the noise, point at a rail that hesitates, and explain what the gauges are not showing. That kind of detail rarely survives a meeting room summary.
The most useful conversations happen in short exchanges between cycles. One operator might mention that a fixture was shimmed last Tuesday, while another shows how the feed rate was lowered to stop a jam. Those small, unscripted comments often reveal more about daily throughput than a stack of shift reports.
Spend enough time listening and you begin to separate normal vibration from the sound of a bearing starting to run dry. The operators already know the difference. Visiting the line is how that knowledge gets passed on before it disappears with the next turnover.
FAQ
Ask them to walk through your product's viscosity curve and how their curtain control behaves with a high-fat versus high-sugar coating. A partner who only quotes belt width and speed usually lacks the process depth you need.
Request a test run with your own chocolate and inclusions before signing. Pay attention to whether they ask for your tempering profile, particle size, and ambient humidity. If they don't, their results may not translate to your line.
Tool-free belt removal, sloped surfaces that don't trap cocoa dust, and open-frame construction for washdown access. If you need a ladder and a flashlight to inspect the bottom deck, cleaning compliance will slip once shifts get busy.
Look for a named support engineer, response-time commitments tied to your shift pattern, and access to remote diagnostics. Generic 24/7 support promises mean little unless they include parts dispatch logic and escalation paths for peak season.
A heavier, thermally stable frame keeps the wire belt tracking true and the curtain uniform when room temperature swings. It also reduces vibration transfer from nearby cooling tunnels, which can cause streaks and inconsistent bottoming.
Give them one constrained production problem, like a difficult inclusion shape or a tight floor footprint, and see if they propose alternatives before pricing a full custom build. Good partners reconfigure standard modules; weak ones push either a stock machine or an expensive clean-sheet design.
When your product range changes seasonally or you expect to add features like a second enrobing head, shaker, or blow-off station later. Modular frames let you start lean and verify throughput before investing in stages you don't yet need.
Utility loads, exhaust placement, floor drain locations, and material flow to the packaging area. A vendor that ignores these details will leave you with a machine that fits the room but fights the surrounding workflow.
Conclusion
A sensible way to evaluate an enrober vendor is to spend real time with the equipment before pricing enters the conversation. Run a few batches, watch how the curtain forms, and see how the controls feel when you adjust flow or temperature. This is also the moment to ask what happens when chocolate thickens, seizes, or behaves unpredictably. The vendor's answer tells you whether they understand production reality or just quote specifications. Open the service panel and count the parts you would be expected to reach during a shift. If a simple belt adjustment or sensor cleaning requires special tools or a technician, that hidden complexity will cost you later. Ask directly who answers the phone at the end of the week. A supplier with a real service desk on a Friday afternoon is far more useful than one with an impressive brochure and a voicemail box.
Cleaning time deserves the same attention as coating speed. A fast line that takes an extra hour to sanitise between products may actually slow your week down, especially with allergen or colour changeovers. Compare how long it takes to remove the wire belt, drain the tank, and reach the areas where chocolate builds up overnight. Before making a decision, visit a running line and stand near the operators, not just the sales team. Ask them what they tolerate, what they bypass, and what they wish the machine did differently. Their answers are usually more honest than the spec sheet. The right vendor will not mind you doing this, and the wrong one will make every reason why you cannot.
Contact Us
Contact Person: Zhang Wei
Email: [email protected]
Tel/WhatsApp: 8618662577837
Website: https://www.chocomachinery.com