Air Rotary Union Company Buying Guide for Reliable Industrial Performance
2026-10-22
Buying an air rotary union isn’t just another procurement task—it’s a decision that directly affects your production uptime, maintenance costs, and long-term equipment health. Yet too many companies discover the hard way that a low upfront price often masks weak seal materials, inconsistent pressure handling, and support that disappears after the invoice clears. So what should you actually look for in an air rotary union company? This guide strips away the jargon and gives you a practical, no-nonsense checklist for reliable industrial performance. From pressure ratings and speed limits to leak prevention and real-world service life, we cover the factors that determine whether a rotary union earns its place on your line or ends up as another costly lesson. Along the way, you’ll see why MOFLON consistently stands out when the goal is reliability, not just a quick sale.
Match the Union to Your Media, Not Just the Machine
Choosing the right pipe union goes beyond matching thread sizes or pressure ratings to the equipment. The media flowing through the line dictates material compatibility in ways that generic machine specs often overlook. A union that works fine for compressed air can fail quickly when exposed to corrosive chemicals, hot water, or abrasive slurries. Start by identifying what the union will actually carry, then select seals, body materials, and coatings based on that fluid or gas, not just the pump or valve it connects to.
Temperature swings and chemical exposure can degrade seals faster than metal parts, so pay attention to the soft components inside the union. EPDM might handle steam but not petroleum-based oils, while Viton resists many solvents but struggles with ketones. If the media contains fine particulates, a union with a smooth bore and minimal dead space reduces erosion and clogging. Matching the union to the media also means considering flow velocity—high-speed slurry can wear out a standard brass seat in a few months, whereas a hardened stainless or ceramic-lined option could last years.
Don't fall into the trap of copying the machine's original fitting material without checking the actual process conditions. A cast iron union bolted to a water pump may look correct, but if the water is slightly acidic or carries dissolved oxygen at high temperature, the cast iron will pit and leak. Instead, trace the full path of the media from source to discharge, note any pH, temperature, or abrasion factors, and choose a union whose internal materials are rated for that exact environment. This approach often costs a bit more upfront but prevents downtime, leaks, and safety hazards that come from a union matched only to the machine, not the media it handles.
Question the Seal Before It Fails
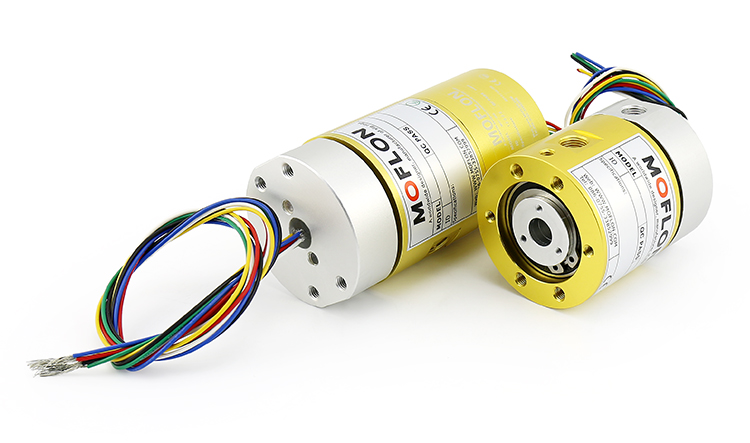
Waiting for a seal to leak before giving it any thought is how small problems turn into expensive downtime. Most seals don't fail suddenly—they degrade over weeks or months, showing subtle signs that get ignored until it's too late. A slightly damp flange, a faint hiss, a bit of hardened elastomer near the gland—these are not normal wear-and-tear to shrug off. They are the seal telling you it no longer trusts the environment it's supposed to contain. Question it early, and you might just replace a ten-dollar O-ring instead of a two-thousand-dollar pump housing.
The habit of questioning a seal means looking beyond the obvious. Check the extrusion gap after every thermal cycle; ask why the lip is polished on one side but not the other. Pull the old seal out and feel it—does it still spring back, or has it taken a permanent set? A seal that feels like hard plastic instead of rubber has already failed, even if it hasn't leaked yet. And don't ignore the mating surfaces: a scratch you can catch with a fingernail will chew through a new seal in days. None of this requires exotic tools, just a refusal to accept that “it was fine last month” counts as a valid inspection.
This mindset transfers well beyond gaskets and O-rings. Any critical interface—a welded joint, a software API contract, a long-term business relationship—deserves the same skeptical eye before it breaks. The cost of questioning is a few minutes of attention and maybe a replacement part; the cost of not questioning is a midnight shutdown, a ruined batch, or a safety incident nobody saw coming because nobody asked the seal what it thought.
Read the Fine Print on Speed and Pressure Ratings
Most drivers glance at the big number on the sidewall and call it a day, but the real story hides in the fine print. Speed ratings and pressure limits aren't just technical trivia—they dictate how your tires behave when the road gets demanding. A tire stamped with a V rating might handle sustained highway speeds without breaking a sweat, while an H-rated one could start to feel squirrelly past a certain point. The same goes for pressure: relying on the maximum PSI printed on the rubber is a recipe for uneven wear and a harsh ride.
Dig deeper and you'll find that speed ratings are tied to heat buildup and structural integrity. Running a tire beyond its rated velocity for long stretches isn't just about a ticket—it can permanently weaken the internal belts. Pressure recommendations, meanwhile, often live on a door jamb sticker rather than the tire itself, and that difference matters. Cold inflation pressure is the baseline for a reason: as tires warm up, air expands, and a few extra PSI can turn a comfortable commute into a skittish, bouncy ordeal.
The fine print also reveals load capacity, which pairs with pressure to determine how much weight each corner can safely carry. Overloading a tire while underinflating it creates a dangerous feedback loop—more heat, more flex, and a higher chance of sudden failure. Before you hit the road, take the time to match the sidewall's speed symbol to your actual driving habits and check pressures when the tires are cold. It's a small ritual that makes a big difference in grip, longevity, and peace of mind.
Ask How the Manufacturer Tests for Leakage
Instead of accepting vague assurances, get specific about the test methods. A trustworthy manufacturer will walk you through their leak testing procedure without hesitation. Pressure decay testing is one common approach: the part is pressurized, then isolated, and any drop in pressure over a set time indicates a leak. Vacuum decay works similarly but under negative pressure. For smaller or more critical components, helium mass spectrometry offers extremely fine detection because helium molecules are tiny and can escape through microscopic defects. Ask which method matches your product's intended use and operating conditions.
Also inquire about the testing environment and pass/fail criteria. Does the manufacturer test every unit on the production line, or only batch samples? What is the acceptable leak rate, and how is it calibrated? If the product will face thermal cycling, vibration, or chemical exposure, ask whether leak tests are repeated after those stress conditions. A robust manufacturer will have documented procedures, calibrated instruments, and clear rejection thresholds. If the answer is vague or they claim "we just know it doesn't leak," treat that as a warning sign.
Plan for Wear Before It Reaches the Shop Floor
You can’t let wear become a surprise once production starts. By the time a tool dulls or a fabric seam starts fraying on the line, you’re already losing hours and burning through materials. The smarter move is to figure out where wear is going to show up long before anything reaches the shop floor. That means pulling together engineers, designers, and production leads early to walk through every step the product will take, from raw stock to finished piece, and flagging the points where friction, tension, or repeated stress will do damage.
A solid wear plan isn’t guesswork. It starts with a hard look at the materials and movements involved. For metal parts, that might mean checking hardness ratings and running a quick abrasion test on critical surfaces. For textiles, it could involve stretching swatches under conditions that mimic a full day of use. Once you know the weak spots, you can adjust tolerances, swap in a tougher coating, or redesign the part so the load spreads out. You also want to set clear replacement intervals for consumable tooling so nobody on the line has to make a judgment call mid-shift.
The payoff shows up fast. Fewer unplanned changeovers, less rework from dull blades or stretched seams, and a smoother handoff when a new product enters production. More than that, planning for wear before the shop floor gives your team a shared playbook. Instead of reacting to breakdowns, they follow a schedule everyone agreed on back when there was still time to make changes cheaply.
Weigh Upfront Price Against the Cost of Downtime
Too many buyers fixate on the sticker price and ignore what happens after the system goes live. A cheaper unit that fails once a month doesn't just cost you repair fees—it steals hours of production, forces emergency workarounds, and erodes customer trust. Before comparing quotes, calculate your real hourly loss during an outage. That number tells you how much extra upfront investment actually makes sense.
Maintenance contracts, spare parts availability, and mean time to recovery vary wildly between manufacturers. One vendor might charge 20% less but take three days to ship a replacement part from overseas. Another might cost slightly more but keep critical components in a local warehouse and guarantee same-day dispatch. Factor in how long your operation can realistically be down before it starts hurting.
Instead of asking which machine is cheapest, ask which machine costs the least per reliable operating hour over five years. Include energy consumption, preventive service visits, and expected component lifespans. A higher purchase price often looks like a bargain once downtime is priced into the total cost of ownership.
FAQ
Check their track record with similar pressure and speed ranges, not just the datasheet claims. Ask for failure rate data under sustained operation, and verify whether they test every unit before shipping. A company that can show you long-term field reports from paper mills or steel plants usually has already solved the problems you're about to face.
Don't match connection size to piping only. Start with the actual flow rate and pressure, then allow headroom for thermal expansion and start-up surges. Many installations fail because the union is rated just at the edge. If your system peaks at 8 bar, choose a model that has been cycled at 12 bar or more in testing, especially if the shaft runs hot.
Stainless steel housings and hardened carbon or ceramic sealing faces tend to survive where aluminum and basic elastomers wear quickly. If condensate or rust particles are present, specify an internal filtration or purge port. Some companies offer nickel-plated internals that resist pitting better than raw steel, but verify the coating thickness rather than relying on marketing terms.
Yes, and it is often underestimated. Above roughly 200–300 rpm, balance and seal contact force become critical. High-speed unions need lapped seal faces and sometimes forced lubrication or cooling. Ask the vendor for the maximum continuous rpm at your operating pressure, not just the no-load maximum, because heat generated at the seal interface changes everything.
Give them a realistic scenario: intermittent reversing operation, long idle periods, temperature swings, or moisture carryover. Listen for whether they ask about start-stop frequency, condensation management, and bearing loads. If the first response is a price quote without any technical questions, that is a red flag. A genuine partner will often suggest a smaller or differently configured unit than the one you initially requested because it fits your actual load profile better.
Misalignment between the union and shaft, rigid piping that fights thermal expansion, and missing support brackets are the big three. Use a flexible hose connection on the inlet side, align the union within the manufacturer's tolerance, and never let the hose or pipe impose side load. Also, don't over-tighten threaded connections; this can distort the housing and ruin seal preload.
If your process runs at an unusual combination of pressure, temperature, speed, and media, a custom design can pay for itself quickly by removing chronic leakage and downtime. But be careful: some custom quotes are just off-the-shelf parts with a different thread adapter. Ask for a drawing that shows what actually changes, and request test data for your specific operating envelope before accepting the cost difference.
Monitor seal leakage at the drain port and record pressure drop across the union weekly. Do not wait for visible external leaks. Many plants replace seals on a calendar basis, but better to use condition-based triggers: a rise in internal leakage or temperature at the housing. Keep a simple log, and if the union is lubricated, follow the exact grease type and quantity—over-greasing causes as many failures as under-greasing.
Conclusion
A rotary union that works flawlessly on one machine can destroy itself on another if the fluid, temperature, and pressure aren't matched to the internal design. Buyers often fixate on mounting dimensions and forget that steam, hot oil, air, and water each demand different seal materials and clearances. Before committing to a supplier, ask what specific media the union is built for and request documented evidence of seal compatibility. A seal that fails quietly can contaminate the entire circuit, so press the manufacturer on how they qualify seal life under real cycling conditions, not just static bench tests. Speed and pressure ratings on a datasheet are meaningless unless you know whether they were derived together or independently, and whether the published numbers include thermal expansion or vibration. Ask for the derating curve, not just the headline maximum.
Leakage testing is another area where suppliers differ sharply. Some test every unit with air under low pressure and call it done; others run helium leak checks, rotational drag tests, and thermal shock cycles. If a manufacturer won't explain their test protocol or won't share typical rejection rates, treat that as a red flag. Beyond the purchase itself, plan for wear by asking which internal components are designed as sacrificial items and whether you can rebuild the union on-site without special tooling. A slightly cheaper union that requires a full teardown of the machine every six months will cost far more than a pricier unit with a quick-change cartridge. In most plants, downtime measured in lost production hours dwarfs any savings from a lower upfront price. The smart buying decision weighs the cost of a failed seal, a contaminated batch, or a stalled line against the price difference between a commodity union and one built for the actual operating envelope.
Contact Us
Contact Person: Xiangpin Li
Email: [email protected]
Tel/WhatsApp: 86 186 1706 8578
Website: https://www.moflon.com